Choosing among China’s top absorbable surgical suture manufacturers requires more than comparing factory photographs or product catalogs. This market includes established medical-device producers, specialized suture factories, and suppliers serving private-label brands. Their capabilities may differ significantly. Some focus on fast production, while others emphasize research, sterile packaging, or customized needle designs. This guide introduces manufacturers that deserve closer evaluation when sourcing Absorbable Surgical Sutures for hospitals, distributors, and medical-device companies.
Practical assessment should begin with material quality, tensile-strength retention, knot security, and predictable absorption behavior. Manufacturing experience matters, especially when products must remain consistent across different batches. Look for documented quality systems, validated sterilization processes, traceable raw materials, and clear technical files. Certifications can support credibility, but they should never replace independent verification. A supplier may display impressive certificates yet provide limited production evidence. That is a warning sign.
Ask for samples. Review the needle’s curvature, suture handling, packaging seal, and labeling accuracy. Speak with quality managers, not only sales representatives. Reliable manufacturers should explain inspection procedures without vague promises. They should also describe how complaints, nonconformities, and product changes are managed. No supplier is perfect. Even experienced factories can face delays, material variations, or communication gaps. That reality deserves attention.
The strongest candidates combine engineering knowledge, stable production, transparent documentation, and responsive support. Still, rankings should remain flexible. A manufacturer suitable for general surgery may not fit ophthalmic, dental, or veterinary applications. Careful comparison, on-site audits, and professional regulatory review can turn a promising supplier into a dependable long-term partner.
Absorbable surgical sutures are sterile threads designed to support healing tissues before gradually breaking down inside the body. Unlike non-absorbable sutures, they usually do not require removal. Natural materials are digested by tissue enzymes, while many synthetic materials degrade through hydrolysis. The absorption period can range from several days to many months.
These sutures are used for closing internal tissues, repairing muscle, securing blood vessels, and closing selected skin wounds. A surgeon considers tissue strength, healing speed, wound tension, and infection risk before choosing a suture. For example, rapidly healing mucosa may need short-term support, while fascia often requires longer strength retention. Needle shape and thread flexibility also affect handling during surgery.
Small details matter. A suture that feels smooth can reduce tissue drag, yet it may be harder to control with wet gloves. Secure knots matter too. One overlooked issue is swelling around the wound, which can change how the material performs. Absorbable does not mean universally better. Patient health, tissue condition, and surgical technique remain important. Clinical protocols and professional training should guide selection, because no single material suits every procedure.
Identifying China’s top absorbable surgical suture manufacturers requires more than comparing prices. Grand View Research estimated the global absorbable sutures market at about USD 2.5 billion in 2023, with continued growth expected through 2030. This demand increases the importance of stable production, not merely attractive quotations.
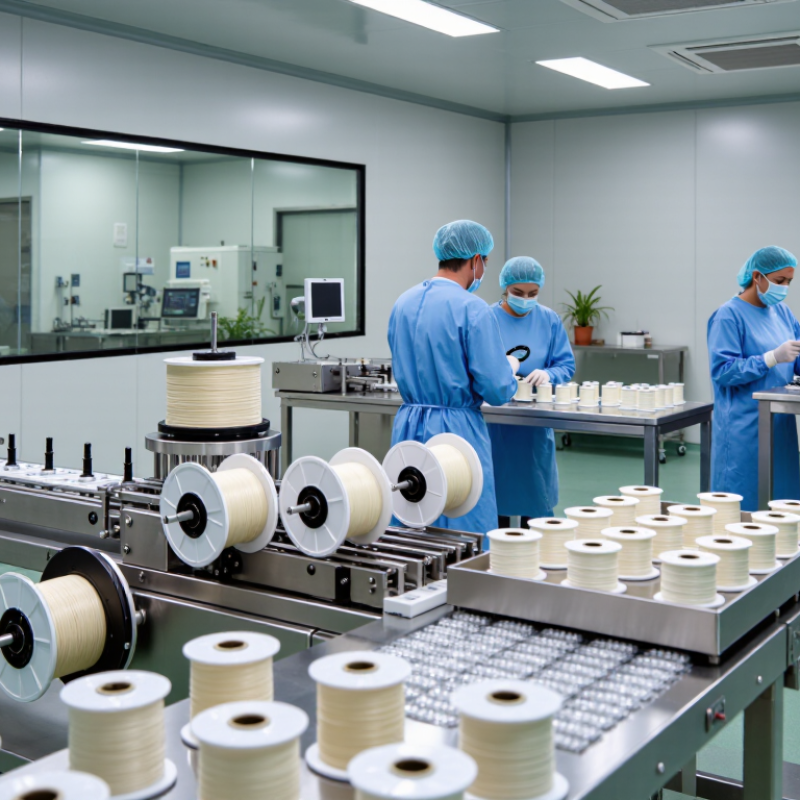
Experienced buyers should inspect cleanrooms, polymer storage, needle attachment, and final packaging. Batch-level traceability matters. Ask for tensile-strength results, absorption profiles, sterility validation, and shelf-life evidence.
ISO 13485 certification is useful, but it does not replace factory-level verification.
Reliable manufacturers should also provide biocompatibility assessments under ISO 10993 and quality records aligned with applicable USP requirements. The World Health Organization’s Global Patient Safety Action Plan 2021–2030 highlights preventable harm as a major healthcare concern. Suture consistency directly supports safer wound closure.
Request samples from several production batches, then compare knot security, handling, needle penetration, and break strength. A polished certificate wall can still hide weak process control. I have seen specifications look excellent on paper, yet feel inconsistent during handling. That deserves a second review.
Tips:
Visit the facility when possible. Check environmental monitoring records, sterilization indicators, complaint handling, and recall procedures. Confirm whether test reports come from qualified laboratories. Review export experience for your target market, but do not treat export volume as clinical proof. No checklist is perfect. Combine documents, physical samples, audit findings, and transparent technical communication before selecting a long-term supplier.
Leading Chinese absorbable suture manufacturers typically offer broad product lines for general surgery, gynecology, orthopedics, and wound closure. Their catalogs may include braided and monofilament sutures made from PGA, PGLA, PDO, or absorbable natural materials. Common options include 3-0 and 4-0 sizes, reverse-cutting needles, and pre-attached sterile needles.
Manufacturing quality depends on more than raw material selection. Experienced facilities control polymer purity, tensile strength, needle attachment, sterilization, and package integrity. Many operate under ISO 13485 quality systems and provide batch records, technical files, and test reports for customer review. Hospitals and distributors should verify these documents independently. A polished catalog is not enough.
Product details matter in real operating rooms. A braided suture may handle smoothly, while a monofilament can reduce tissue drag. Needle curvature, memory, coating, and absorption time also affect surgical performance. Some Chinese suppliers support private-label packaging, custom needle combinations, and different carton quantities. That flexibility helps procurement teams, but it can complicate quality consistency.
One practical concern is communication after shipment. Clear instructions for storage, shelf life, complaints, and traceability should be available before purchase. Manufacturers that welcome clinical feedback usually show stronger professional maturity. Still, no supplier is perfect. Product claims should be checked against applicable registration requirements, validated testing, and actual surgical needs.
China’s leading absorbable surgical suture manufacturers are judged by more than production volume. Quality begins with controlled raw materials, documented procedures, and trained inspection teams. Manufacturers should operate under ISO 13485 quality management systems. Their facilities need traceability from polymer lots to finished packages. Every batch should have clear records.
Practical evaluation includes checking suture diameter, tensile strength, needle attachment, knot security, and absorption behavior. Testing may follow applicable pharmacopeial requirements and ISO 10993 biological evaluation principles. Sterile products also require validated sterilization processes and stable packaging seals. Certifications should be verified through current certificates, audit records, and product scope. A certificate alone proves little.
Experienced factories often use controlled environments, automated braiding equipment, and calibrated testing instruments. They should provide samples, technical files, stability data, and certificates of analysis. Manufacturing capability also includes cleanroom discipline, batch release procedures, complaint handling, and recall readiness. Ask how deviations are investigated. The answer reveals maturity. Even capable manufacturers can have weak documentation or inconsistent subcontractor controls. This deserves careful review. A reliable supplier communicates limitations clearly and accepts independent testing when needed. Great equipment helps, but disciplined people protect patient safety.
| Evaluation Dimension | Recognized Standard or Regulatory Reference | Objective Requirement | Relevant Manufacturing Capability | Recommended Verification Evidence |
|---|---|---|---|---|
| Quality management system | ISO 13485:2016; applicable Chinese medical-device regulations | A documented medical-device quality system covering design, purchasing, production, testing, traceability, complaints, and corrective actions. | Controlled procedures, trained personnel, batch records, nonconformance management, and CAPA processes. | Valid certificate issued by an accredited certification body, audit reports, quality manual, and sample batch documentation. |
| Product registration and market access | National Medical Products Administration requirements; destination-market regulations | The finished suture must be legally registered or authorized for the intended market and product classification. | Regulatory documentation, technical files, risk management, clinical or performance evidence, and post-market surveillance. | Registration or authorization documents, product specifications, labeling files, and regulatory inspection records. |
| Absorbable material selection | Applicable pharmacopeial monographs and biocompatibility requirements | Material identity, purity, molecular characteristics, coating composition, and absorption behavior must be defined and controlled. | Processing of synthetic absorbable polymers such as polyglycolide, polydioxanone, polyglactin-type materials, or validated natural absorbable materials. | Raw-material certificates, identity testing, supplier qualification, material specifications, and finished-product release records. |
| Suture diameter and size control | Applicable United States Pharmacopeia or European Pharmacopeia suture requirements | Diameter must remain within the declared tolerance for the selected suture size and construction. | Precision extrusion, drawing, braiding, twisting, coating, calibrated measurement, and in-process inspection. | Dimension specifications, calibrated measuring equipment, sampling plans, and batch test results. |
| Tensile strength and knot performance | Applicable pharmacopeial suture tests and validated internal methods | Straight-pull strength, knot-pull strength, knot security, and strength retention must meet the declared product specification. | Controlled filament formation, braid or twist consistency, coating control, needle attachment, and mechanical testing. | Validated test methods, calibrated tensile testers, lot-release reports, and strength-retention data over the claimed absorption period. |
| Needle and suture attachment | Applicable pharmacopeial requirements and approved product specifications | The attachment must withstand the required pull force and maintain a smooth, clinically suitable transition between needle and thread. | Automated or controlled swaging, laser-drilled or drilled needle compatibility, needle-point finishing, and attachment-force inspection. | Needle material certificates, attachment-force test records, visual inspection criteria, and validated assembly procedures. |
| Biocompatibility evaluation | ISO 10993 series | Biological safety must be assessed according to the device’s materials, tissue contact, contact duration, sterilization method, and degradation products. | Material characterization, extractables assessment, degradation evaluation, toxicological review, and risk-based biological testing. | Biological evaluation plan and report, chemical characterization, test reports from qualified laboratories, and risk-management linkage. |
| Sterilization process | ISO 11135 for ethylene oxide; ISO 11137 for radiation sterilization, where applicable | The validated sterilization process must achieve the specified sterility assurance level without damaging the suture or packaging. | Validated sterilization cycles, controlled environmental conditions, residual testing where applicable, and routine process monitoring. | Validation protocols, dose or cycle records, biological indicators where applicable, sterility testing, and residual sterilant reports. |
| Cleanroom and environmental control | ISO 14644 series; applicable contamination-control procedures | Controlled particle levels, air pressure, temperature, humidity, personnel practices, and cleaning procedures must be maintained. | Classified production and packaging areas, gowning procedures, environmental monitoring, and documented cleaning validation. | Cleanroom classification reports, environmental monitoring trends, calibration records, and cleaning-validation documents. |
| Packaging and sterile barrier system | ISO 11607 series | Packaging must protect the product, maintain sterility until use, and withstand transportation and storage conditions. | Validated sealing, pouch or tray forming, label control, packaging-integrity testing, and transport simulation. | Seal-strength results, dye-leak or integrity testing, accelerated-aging data, transport testing, and packaging validation reports. |
| Microbiological testing and sterility assurance | ISO 11737 series and applicable pharmacopeial sterility requirements | Bioburden, sterility, and microbiological control must be assessed using validated methods appropriate to the product and process. | Defined bioburden limits, routine microbiological monitoring, controlled laboratory practices, and release authorization. | Bioburden trends, sterility test reports, laboratory qualification records, and sterilization validation documentation. |
| Absorption and degradation profile | Approved product specification; validated degradation and strength-retention methods | The declared absorption period and mechanical-strength retention must be supported by product-specific laboratory and, where required, clinical evidence. | Controlled polymer characteristics, hydrolysis or enzymatic-degradation studies, and stability monitoring. | In-vitro degradation data, strength-retention curves, molecular-weight testing, stability reports, and approved labeling claims. |
| Risk management and process validation | ISO 14971:2019; ISO 13485:2016 | Manufacturing and product risks must be identified, controlled, verified, and reviewed throughout the product life cycle. | Validated extrusion, braiding, coating, needle attachment, packaging, sterilization, and software-controlled inspection processes where applicable. | Risk-management file, process-validation protocols, equipment qualification, change-control records, and process-capability data. |
| Traceability and supply-chain control | ISO 13485:2016; applicable regulatory traceability requirements | Each production lot should be traceable to raw materials, processing equipment, operators, inspection results, packaging, and distribution records. | Unique lot numbering, electronic or controlled paper records, qualified suppliers, incoming inspection, and recall readiness. | Traceability exercise results, supplier-audit reports, incoming-inspection records, batch-history records, and mock-recall documentation. |
| Product range and customization | Approved product specifications and applicable market requirements | Available sizes, lengths, needle geometries, coatings, colors, and packaging configurations must be clearly specified and validated. | Capability to produce monofilament or braided constructions, multiple USP size ranges, various needle profiles, and customized sterile packaging. | Product catalog, technical drawings, approved samples, customization change-control records, and conformity test reports. |
| Shelf-life and storage stability | ISO 11607-related packaging validation; applicable stability and labeling requirements | The product must retain specified sterility, packaging integrity, mechanical performance, and labeling accuracy throughout the claimed shelf life. | Real-time and accelerated-aging studies, controlled storage conditions, expiry-date assignment, and ongoing stability programs. | Stability protocols, aging reports, seal-integrity results, storage instructions, and documented shelf-life rationale. |
The criteria above are industry-level evaluation benchmarks. Specific requirements, test limits, certification scope, and regulatory obligations should be confirmed against the intended suture material, product configuration, and destination market.
How to Choose the Right Chinese Absorbable Suture Manufacturer
Choosing a Chinese absorbable suture manufacturer requires more than comparing prices. Start by checking ISO 13485 certification, documented quality procedures, and product registration records for your target market. Ask for the manufacturer’s scope of certification. It should cover the actual suture type, material, and sterile configuration you plan to purchase.
Request technical evidence, not polished promises. Review tensile strength data, knot security results, needle attachment testing, and absorption profiles for each size. Pay attention to sterilization validation and packaging integrity. A reliable factory should provide batch traceability, raw material records, and clear deviation procedures. Sample evaluation matters. Inspect needle smoothness, thread memory, coating uniformity, and package labeling under normal handling conditions.
Communication reveals operational maturity. Can the technical team explain differences between absorbable polymers? Do they answer questions with test methods and acceptance limits? Ask about production capacity, minimum order quantities, lead times, and change-control procedures. A factory may offer an attractive quote, but unstable material supply can create expensive delays. That risk is easy to underestimate.
Visit the facility when possible, or use an independent audit. Check cleanroom practices, calibration records, operator training, and final inspection areas. Do not rely on certificates alone. Documents can be current while daily execution remains inconsistent. A staged order with defined quality checkpoints is often safer than a large first purchase. Leave room for doubt, because even a professional supplier can make an avoidable mistake.
A practical reference for evaluating Chinese absorbable surgical suture manufacturers and selecting the appropriate material.
Values show approximate complete absorption periods commonly reported for standard absorbable suture materials. Actual performance may vary with polymer formulation, tissue condition, suture size, sterilization, and storage. When comparing manufacturers, also verify tensile-retention profiles, USP compliance, sterilization validation, biocompatibility testing, and traceability.
They are sterile threads supporting healing tissue before gradually breaking down inside the body. Natural materials break down through tissue enzymes. Synthetic materials often degrade through hydrolysis. They usually do not need removal.
Absorption may take several days or many months. The timing depends on the material, tissue location, and product design. Fast-healing mucosa may need short support. Fascia may require longer strength retention.
Surgeons use them for internal tissue closure, muscle repair, and blood vessel support. They can also close selected skin wounds. The choice depends on wound tension and healing speed. One material cannot suit every procedure.
They consider tissue strength, healing speed, infection risk, and surgical technique. Needle shape and thread flexibility affect handling. Swelling around a wound can also change performance. Small details matter.
Braided sutures may feel smooth and handle easily during knot tying. Monofilament sutures can reduce tissue drag. However, smooth threads may become harder to control with wet gloves. The better option depends on the procedure.
Buyers should review raw material control, tensile strength, needle attachment, sterilization, and package integrity. They should also examine traceability from polymer lots to finished packages. A polished catalog is not enough. Ask for samples.
Useful documents include current quality certificates, technical files, stability data, and test reports. Suppliers should provide batch records and certificates of analysis. They should explain complaint handling, recalls, and deviation investigations. Documentation reveals more than equipment alone.
They can test samples for diameter, tensile strength, knot security, needle attachment, and absorption behavior. Sterile products need validated sterilization and stable package seals. Independent verification is sensible. No supplier is perfect.
Absorbable Surgical Sutures are medical closure materials designed to support wound healing and gradually break down inside the body, eliminating the need for removal in many procedures. They are commonly used in soft-tissue approximation, general surgery, obstetrics, gynecology, orthopedics, and other clinical applications. Their performance depends on material composition, absorption time, tensile strength, flexibility, knot security, sterility, and tissue compatibility.
When evaluating China’s leading manufacturers, buyers should examine product consistency, research and development capabilities, production capacity, quality-control systems, and experience serving international markets. Reliable suppliers should provide clear technical documentation, validated sterilization processes, traceability, and appropriate medical-device certifications. Manufacturers may offer different absorbable materials, needle designs, suture sizes, coatings, and packaging options to meet varied surgical requirements. Choosing the right partner requires comparing specifications, testing support, customization capability, delivery reliability, after-sales communication, and compliance with the regulations of the target market.